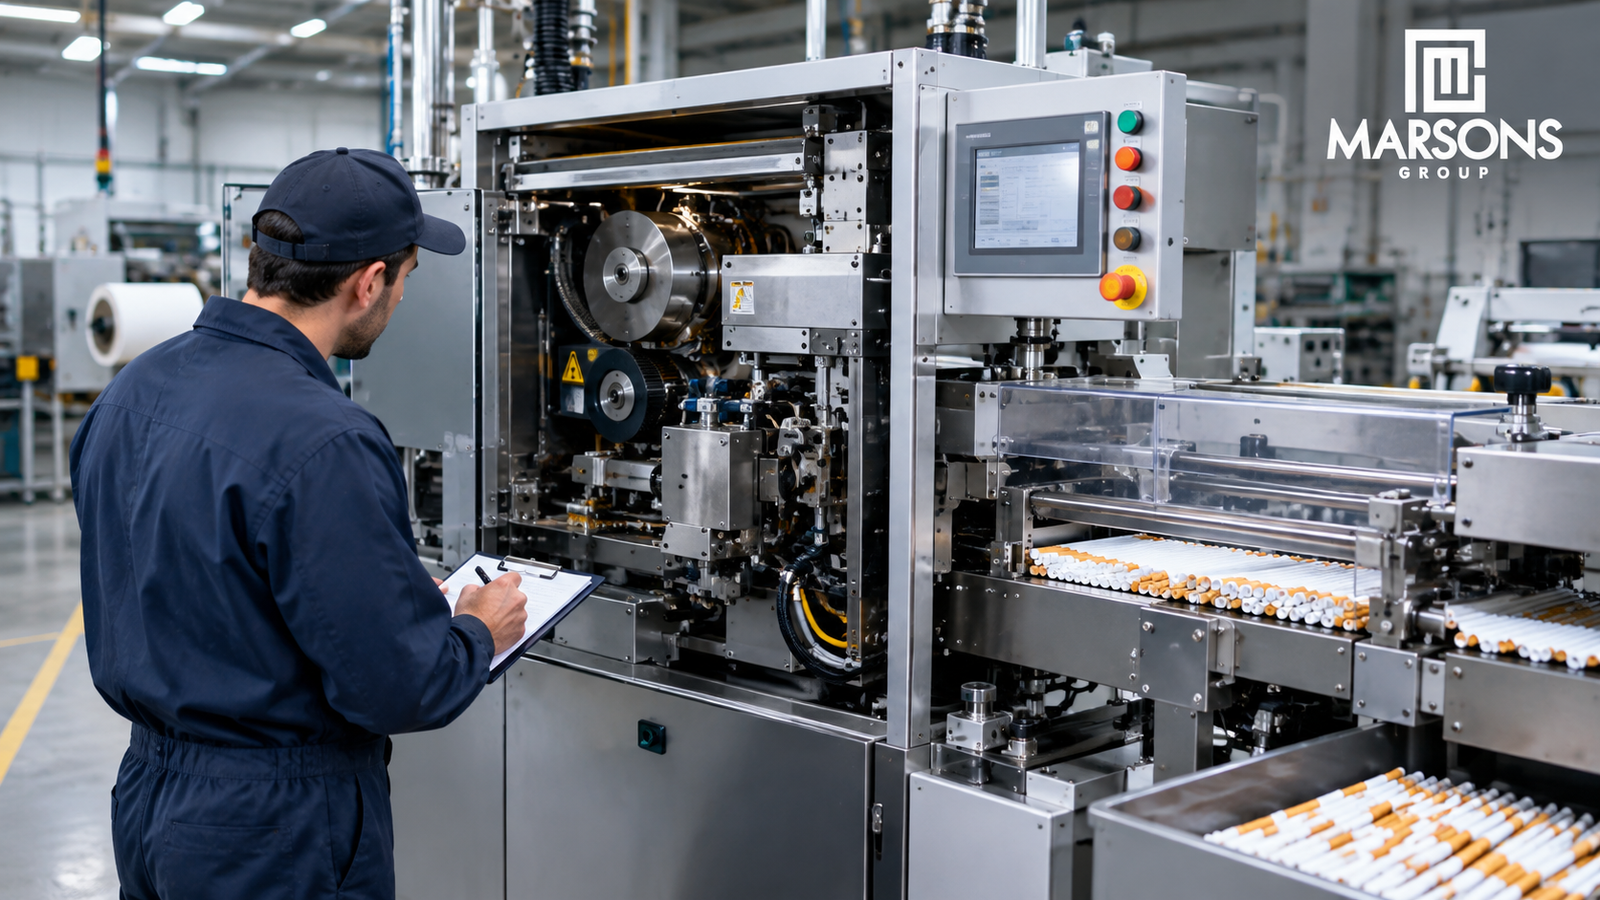
A high speed cigarette maker running at 16,000 cigarettes per minute turns an eight minute stop into more than 128,000 lost units. On lines running closer to 20,000 per minute, a stoppage of five seconds is enough to create a pile-up that takes real time to clear. Industry estimates put tobacco line stoppages at roughly $12,000 to $18,000 per hour in lost output alone, before waste, idle labour and missed delivery commitments are counted. That is why the response to a machine breakdown matters more than the fault itself, and why the service network behind your tobacco machinery for sale decision eventually costs more than the sticker price ever did. The first ten minutes usually decide whether you lose twenty minutes or an entire shift.
The First Ten Minutes: Stabilise Before You Diagnose
Safety and Isolation Come First
Before anyone opens a guard or reaches into the line, the machine must be safe. Hazardous energy control exists because a jammed mechanism can release suddenly and injure the person clearing it, and because unexpected start-up during servicing causes serious harm. Clearing a minor jam during normal production can fall outside full lockout requirements, but only when the task needs no extensive disassembly and the operator is genuinely protected from unexpected activation and stored energy. If those conditions are not fully met, the machine gets isolated and locked out properly. This is not bureaucracy competing with production pressure. An injury turns a thirty minute fault into an investigation, a reportable incident and a line that stays down far longer than the repair ever required.
Protect the Material Still Inside the Line
Once the machine is safe, deal with what is sitting in it. Adhesive contaminates conveyors and any component that contacts paper webs and uniting bands, and it sets while you are diagnosing. Rod sections and filter plugs wedge into guides and flutes, and tobacco left in a hopper or feed system changes moisture the longer it sits. Clearing the affected sections early prevents a simple fault from becoming a strip-down and clean. It also protects the material itself, which carries real cost and, in most jurisdictions, real tax exposure once it becomes waste. Ten minutes spent here routinely saves an hour later, and it can be done by the operator while a technician is still being located.
Capture the Evidence Before It Disappears
The most valuable information about a fault exists in the first few minutes and then evaporates. Record the alarm or fault code exactly as displayed, the reject rate immediately before the stop, the last known good settings, and what changed during the previous run. Note the tobacco batch, moisture reading, paper reel and filter batch. These machine failure first steps cost almost nothing and determine whether the fix is diagnosed or guessed. A single maker can have around 3,000 parameters that are measurable and adjustable, which means an undocumented adjustment during a breakdown can tune the line into a second fault it never originally had. The rule worth enforcing on every shift is simple: write down the current value before you change it, and change one thing at a time.
Triage: Operator Fix, Technician Fix, or Supplier Call?
Triage is where most time is lost, because nobody set a limit in advance. Use a three tier rule with a clock attached. Tier one covers operator-correctable faults such as jams, misfeeds, paper breaks, glue supply and routine cleaning, with a fifteen minute ceiling before escalation. Tier two covers maintenance faults including worn knives, belts, bearings, alignment and sensor errors, with an hour to either restore or diagnose. Tier three is anything involving control systems, drives, structural damage or a fault the team cannot name, and it goes to the supplier immediately rather than after three hours of experimentation. Equipment failure causes roughly 42 percent of unplanned downtime and human error another 23 percent, and unbounded troubleshooting is how that second figure grows.
The Machine That Stopped Is Not Always the Machine That Failed
This is the most commonly missed point on an integrated line. The maker and the packer are coupled, and when the packer jams the maker stops. Teams then spend the first half hour dismantling a maker that is working perfectly. Before diagnosing the stopped asset, check the buffer or reservoir level, the downstream packer and the upstream feed. The same logic applies to environmental causes. Humidity swings in conditioning chambers, cutting rooms and maker halls cause weight variation, poor cut uniformity and inconsistent fill density, so a machine that appears to have failed may simply be receiving material it was never set up to run. Always ask what changed in the material and the room before assuming the mechanism is at fault.
The Most Common Causes of a Cigarette Machine Breakdown
Fault records from maker units cluster into four subsystems: tobacco supply, paper transmission, rod formation and weight control. Recognising the signature shortens diagnosis considerably. Loose ends and empty heads usually point upstream to feed consistency, cut quality or rod density control. Hard rods and weight drift point to trimming and density regulation. Paper breaks and seam failures point to tension, tracking and glue application. Filter tip misalignment points to the tipping section and transfer timing. A rising reject percentage is the warning that precedes most stops, and once rejects cross a set threshold the system will alarm or halt the prime mover automatically. Treating that climbing reject rate as an early fault signal rather than a nuisance is what separates a planned intervention from a full machine breakdown.
When to Escalate to Emergency Repair for Tobacco Machinery
Escalate when the fault is electrical or control related, when the same fault has recurred within a shift, when there is any smell of burning, or when your tier two window has expired without a diagnosis. When you call, have the machine model and serial number, the exact fault code, the production history since the last good run, photographs of the affected section and your parts availability ready. Emergency repair tobacco machinery support is only as fast as the information you provide and the agreement you signed. Check what your coverage actually includes, since parts-only arrangements leave you paying technician time and travel, and some contracts bundle a limited number of on-site visits. Service reach is a purchasing decision as much as a maintenance one, which is why Tobacco Machinery Suppliers Worldwide: How to Verify, Vet & Buy Safely is worth reading before you sign rather than after you break down.
Building a Breakdown Response Plan Before You Need It
Everything above works far better when it is written down in advance. A breakdown response plan should name a trained first responder on every shift, define the three escalation tiers with time limits, list emergency contacts with out of hours numbers, and specify the critical spares held on site. Build that spares list from your own failure history rather than a generic catalogue, because a data-driven spare parts strategy can cut mean time to repair by 40 to 60 percent. Prioritise the twenty or so components most likely to stop production, and weight the list toward long lead time items, since many precision components are imported and can take weeks to arrive. As Marsons Group notes on the supply side, the parts you failed to stock are usually the ones that turn a repair into a shutdown.
Log every stop with duration, root cause and estimated cost. Most plants underestimate unplanned downtime by 40 to 60 percent, and fewer than a quarter know their hourly cost precisely, which means the true figure is often two to four times what management assumes. Logged properly over a few months, the pattern reveals which assets cause most of your losses, and that is what makes prevention fundable. Plants with preventive maintenance completion below 70 percent experience roughly three times more unplanned failures, while structured predictive programmes typically cut unplanned downtime by 30 to 50 percent within the first year.
Knowing When Repair Stops Being the Answer
At some point the repair log becomes the argument. When the same subsystem fails repeatedly, when spares for your model are increasingly hard to source, when a good mean time to repair benchmark of five hours or less is something your line never achieves, and when annual repair spend approaches a meaningful share of replacement cost, the economics have already shifted. Compare a full year of downtime cost, waste, overtime and emergency callout fees against the cost of capital rather than judging each repair invoice in isolation. Operations that run this calculation honestly usually discover the decision was overdue by a year or more, because individual repairs always look cheaper than a machine until they are added up.
Conclusion
When a cigarette machine stops, work the sequence rather than the instinct. Make it safe, clear the material before adhesive and tobacco set, record the fault code and the last known good settings, check whether the failure actually originated downstream or in the material, then triage against a clock rather than against optimism. Change one variable at a time and never adjust a parameter you have not recorded first.
The deeper point is that breakdown response is a preparation problem disguised as a crisis. The plants that recover fastest are not the ones with the best troubleshooters on shift, they are the ones that decide in advance who responds, how long each tier gets, which parts sit on the shelf and when the supplier is called. Write that plan while the line is still running, because nobody writes a good procedure at two in the morning with a stopped maker and a supervisor asking for an estimate.