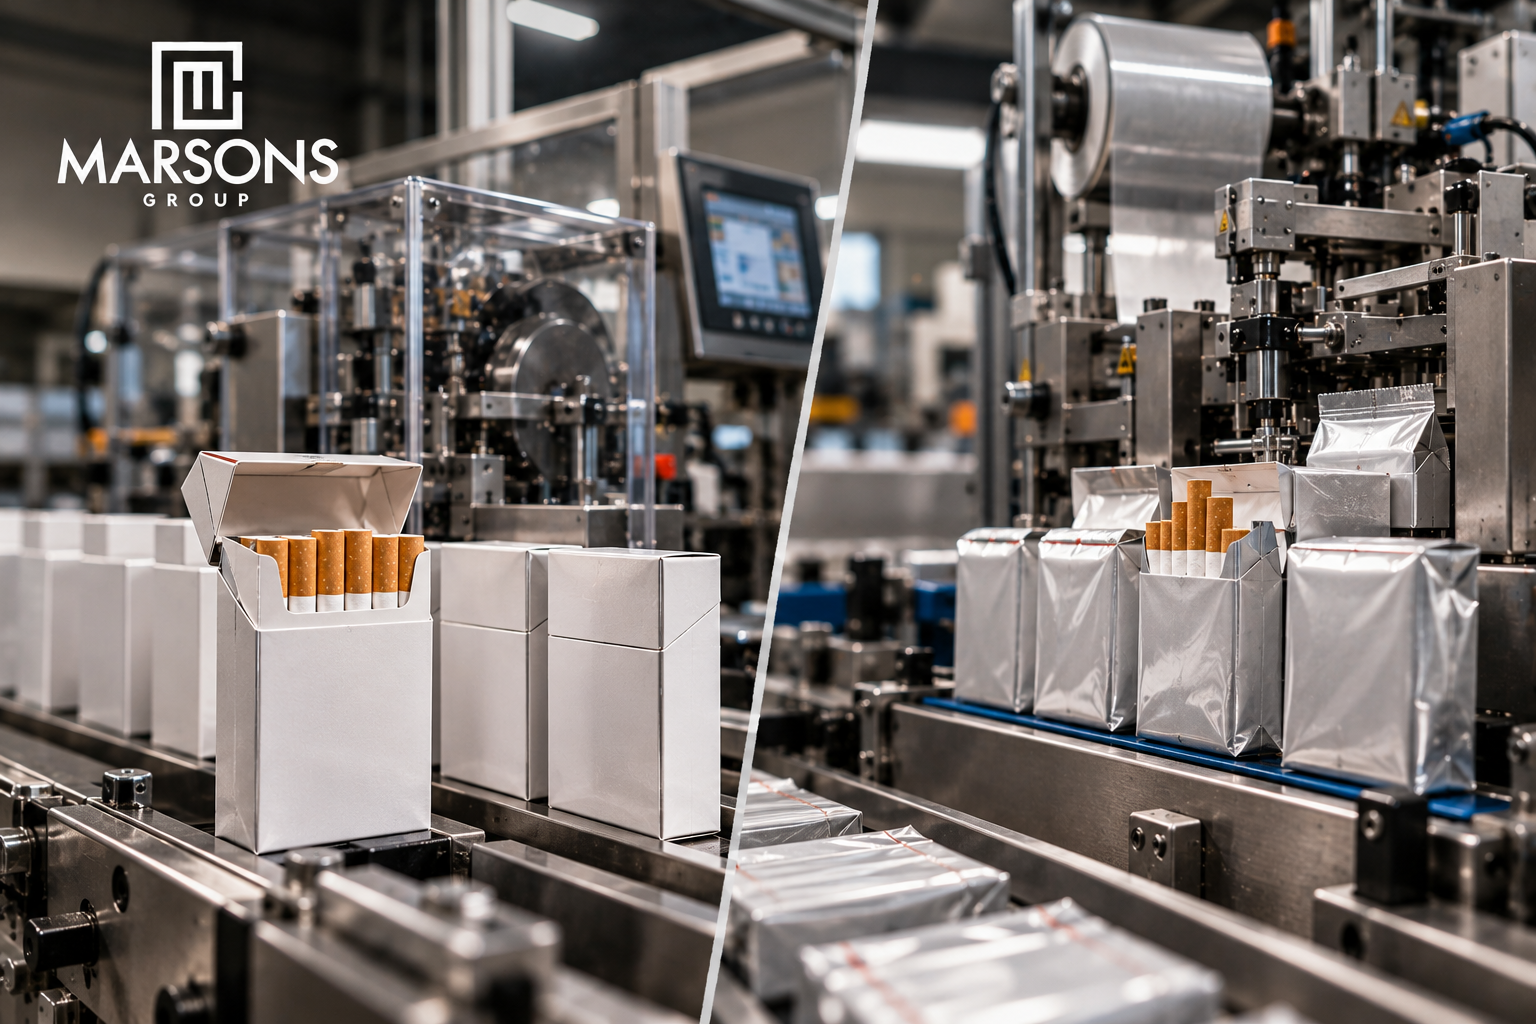
The choice between a hard box line and a soft cup line is one of the few equipment decisions in tobacco manufacturing that locks in your product identity as much as your production capability. It affects material costs on every single unit, determines which export markets you can legally serve, and shapes how your brand sits on a retail shelf. Buyers comparing Cigarette Packing Machines often focus first on packs per minute, yet speed is rarely the variable that decides the outcome. Format demand in your target markets, material economics and regulatory compatibility matter far more. This guide works through the hard pack vs soft pack cigarette packing machine decision in the order a production director should actually approach it.
The Two Formats and What They Demand From Machinery
Understanding the physical construction of each pack explains almost everything about the machines that build them.
How a Soft Pack Is Built
A soft cup pack wraps the cigarette group in an inner foil blank to form a block, then encloses that block in a cup shaped paper outer blank with bottom tabs only, so the foil block projects slightly above the paper cup. The format is defined by comparatively low material consumption. Fewer components mean fewer feed streams, fewer folding stations and a mechanically simpler machine. That simplicity shows up in commissioning time, maintenance demand and the depth of technical skill required on the floor.
How a Hard Box Is Built
A hinge lid box consists of a box part, a lid and a collar, and is a comparatively complex construction. The collar, commonly called the inner frame, is usually produced as a separate blank fed from an additional reel of cardboard. The machine must therefore synchronise cigarette group forming, inner wrapping, blank feeding, collar insertion, multi stage folding and lid closing in one continuous sequence.
Speed Ranges and What Each Class Realistically Delivers
Both formats are available across a wide output spectrum, so speed alone rarely decides the format. Hinge lid packers span roughly 300 to 1,000 packs per minute. Entry and low speed hinge lid machines deliver up to 400 packs per minute and have proven extremely durable in that bracket, with over 1,500 installations worldwide. Mid speed single track machines run at 500 packs per minute, while double track high speed units reach 700. Soft cup packers compete directly at the upper end: a high speed soft cup line runs at 700 packs per minute and can pack up to six million cigarettes in a single eight hour shift under continuous operation. Suppliers also offer intermittent single track soft packers at 500 and 600 packs per minute alongside hinge lid equivalents at identical speeds. The practical implication is that you should not assume one format forces you into a slower line.
Let Your Export Market Decide the Format
This is the section most buyers underweight, and the one most likely to strand an investment. Format preference is not uniform across regions. In a fourteen country pack surveillance study, hard packs accounted for 88.3% of the total sample, with the rectangular non slim shape representing 79.2%. Yet soft pack prevalence reached 52% in Thailand, showing how sharply local demand can diverge from the global average. Choosing format by export market means mapping where your volume will actually be sold over the next five years, not where you sell today. If your growth plan points toward markets where the hard box cigarette format carries premium association and dominates shelf space, a soft pack only line will cap you. If you are supplying price sensitive markets with entrenched soft pack habits, a hard box line adds cost your buyers will not pay for.
Regulation Can Remove the Choice Entirely
Plain packaging regimes do not treat the two formats equally, and the differences between jurisdictions are significant. Australia requires rigid cardboard packs with rectangular surfaces, straight sides and right angles, and permits flip-top lids only, which means soft packs are not permitted there at all. By contrast, the UK, Ireland and France allow carton or soft material and permit cuboid packs with rounded or bevelled edges, so soft packs remain viable across EU markets. The EU Tobacco Products Directive itself imposes partial standardisation covering pack shape, opening style and minimum content. Before signing any purchase order, confirm the pack construction rules in every market on your distribution roadmap. A machine that cannot produce a compliant pack for a target territory is not a cheaper machine, it is a closed door.
Material Consumption and Cost Per Thousand
Soft packs win decisively on material cost, and modern engineering has widened that gap further. A double z-fold design eliminates the need for a separate inner liner without sacrificing product protection, delivering material savings of up to 40%. Hard boxes carry the opposite structural burden: cardboard for the box, an additional reel for the collar, and blank layout wastage that is commercially consequential enough that EC rules have attached a financial penalty to material wasted in packaging print layouts. Run the arithmetic across your annual volume rather than per unit, because a difference measured in fractions of a cent per pack becomes a substantial figure across hundreds of millions of units. Offset that saving against the higher retail price a hard box typically supports before concluding either way.
Brand Positioning and Shelf Presentation
Material savings only matter if the market accepts the format. The flip-top hard box has been used as a brand positioning tool since Philip Morris introduced it in the 1950s to reposition a filtered cigarette brand, and it continues to signal premium quality in most markets. Hard boxes also protect contents from crushing, which matters for distribution channels where packs are handled repeatedly. Soft packs read as economy or traditional depending on the territory, and carry genuine affection in markets where consumers associate the format with established local brands. Neither perception is universal, which is why format should follow market research rather than assumption.
Line Integration and Automation Depth
Whichever format you choose, the packer must be matched to upstream and downstream equipment or the investment underdelivers. Pack wrappers and cartoners are specified to pair directly with packer speeds, typically 500 packs with 50 cartons per minute, 700 with 70, and 1,000 with 100. A mismatch anywhere in that chain creates accumulation or starvation that erodes line efficiency regardless of rated speed. For buyers mapping how these subsystems interact, The Role of Automation in Cigarette Packing Machines in Modern Manufacturing covers the integration logic in more depth. Established suppliers such as Marsons Group generally advise specifying the maker, packer, wrapper and cartoner as a matched complex rather than purchasing stages independently.
Changeover Flexibility and Dual Format Thinking
If your product portfolio is likely to expand, flexibility deserves weight in the decision. Current hinge lid platforms advertise up to 600 packs per minute with full three dimensional conversion completed in a single shift, and format kits that allow rapid changes between lengths such as 83mm and 100mm. Some soft pack complexes can be converted to rigid soft pack production in a few shifts, offering a middle path that delivers hard pack rigidity with soft pack material economics. Ask any prospective supplier for documented changeover times on the exact configuration quoted, and clarify how many format kits are included versus charged separately.
A Practical Decision Framework
Choose a soft pack line if your target markets have established soft pack demand, your competitive position depends on cost per unit, you are not exporting to jurisdictions that mandate rigid packs, and you want lower mechanical complexity with reduced maintenance exposure. Choose a hard box line if you are building a premium or mid-premium brand, exporting to markets where rigid packs dominate or are legally required, or your distribution channels expose packs to repeated handling and crush damage.
Final Conclusion
Start with regulation, because it eliminates options rather than merely ranking them. Then map format demand across your realistic export footprint. Only after those two filters should you compare material economics, speed brackets and changeover flexibility. Both formats are available at competitive speeds from credible suppliers, so the decision rests on where your product will be sold and how your buyers expect it to look and feel in hand.